What Should Buyers Verify During an EV Charger Manufacturer Factory Audit?
Jul 16,2026
Blog
A polished factory tour does not prove that a production line can repeat the same charger build after a component change. Buyers should test serial traceability, incoming-inspection records, second-shift controls, and capacity evidence tied to the exact SKU.
Checklista para auditoria da fábrica de carregadores elétricos—link incoming inspection, controlled assembly, final tests, traceability, capacity, and service records to the exact SKU in the RFQ. ISO 9001 describes a quality-management process; IEC 61851 covers conductive charging functions; IEC 60529 defines specified enclosure ingress tests. None alone proves production capacity or field uptime. Approve a supplier only when records, witnessed tests, and a capacity plan agree.
Before placing a volume order with an EV charger manufacturer, buyers should verify in-house production scope, quality traceability, test records, certification coverage, engineering support, and after-sales readiness through a structured factory audit—not a showroom visit alone.
Part 1. What is an EV charger manufacturer factory audit?
Uma revisão de fornecedores é mais útil quando todas as declarações da fábrica estão vinculadas a um documento ou a um controle testemunhado. Trace a configuração do produto desde a inspeção inicial até a revisão de firmware ou hardware, passando por verificações de processo, testes finais, manuseio de não conformidades, calibração, controle de mudanças e liberação de embarque. Isso cria uma trilha de aquisição pronta para citações, sem presumir que uma visita à fábrica sozinha prove o desempenho no campo. Para o contexto de planejamento público, consulte Requisitos do sistema de carga condutivo IEC 61851-1; O registro de aceitação específico do local ainda controla a decisão final.
Um EV charger manufacturer factory audit is a structured sourcing review that confirms whether a supplier can reliably build, test, document, and support the charger platforms you plan to deploy. It is broader than a product demo because it evaluates process control, not only the sample unit on display.
Buyers typically run audits before first purchase orders, before OEM/ODM branding programs, and before scaling from pilot quantities to recurring project supply.
Audit objective
What good evidence looks like
Weak signal
Production authenticity
Walkthrough of SMT, assembly, burn-in, and final inspection
Marketing office with sample wall only
Quality repeatability
Traveler documents, serial traceability, defect logs
Verbal assurance without records
Engineering depth
Firmware, enclosure, and certification support in-house or controlled
Treat showroom samples as reference units only until production records, test reports, and certification scope are verified for the exact model and power range in your RFQ. (IEC 61851 overview)
How should buyers audit the evidence chain?
Incoming control: sample recent lots for power modules, contactors, cables, connectors, meters, and enclosures. Check approved-vendor lists, inspection criteria, quarantine tags, and disposition of nonconforming parts.
Process control: follow one serial through kitting, torque-controlled assembly, wiring, firmware loading, and burn-in. Confirm calibrated tools, work instructions, first-article approval, ESD controls, and engineering-change records.
Final verification: witness protective, insulation/withstand, functional, communication, and thermal checks on the RFQ configuration. For outdoor models, review the applicable IP test report under IEC 60529; for charging control, confirm the applicable IEC 61851 edition and national deviations.
Feedback loop: reconcile test failures, rework, warranty returns, corrective actions, and firmware releases. A closed-loop record identifies root cause, owner, due date, and effectiveness check.
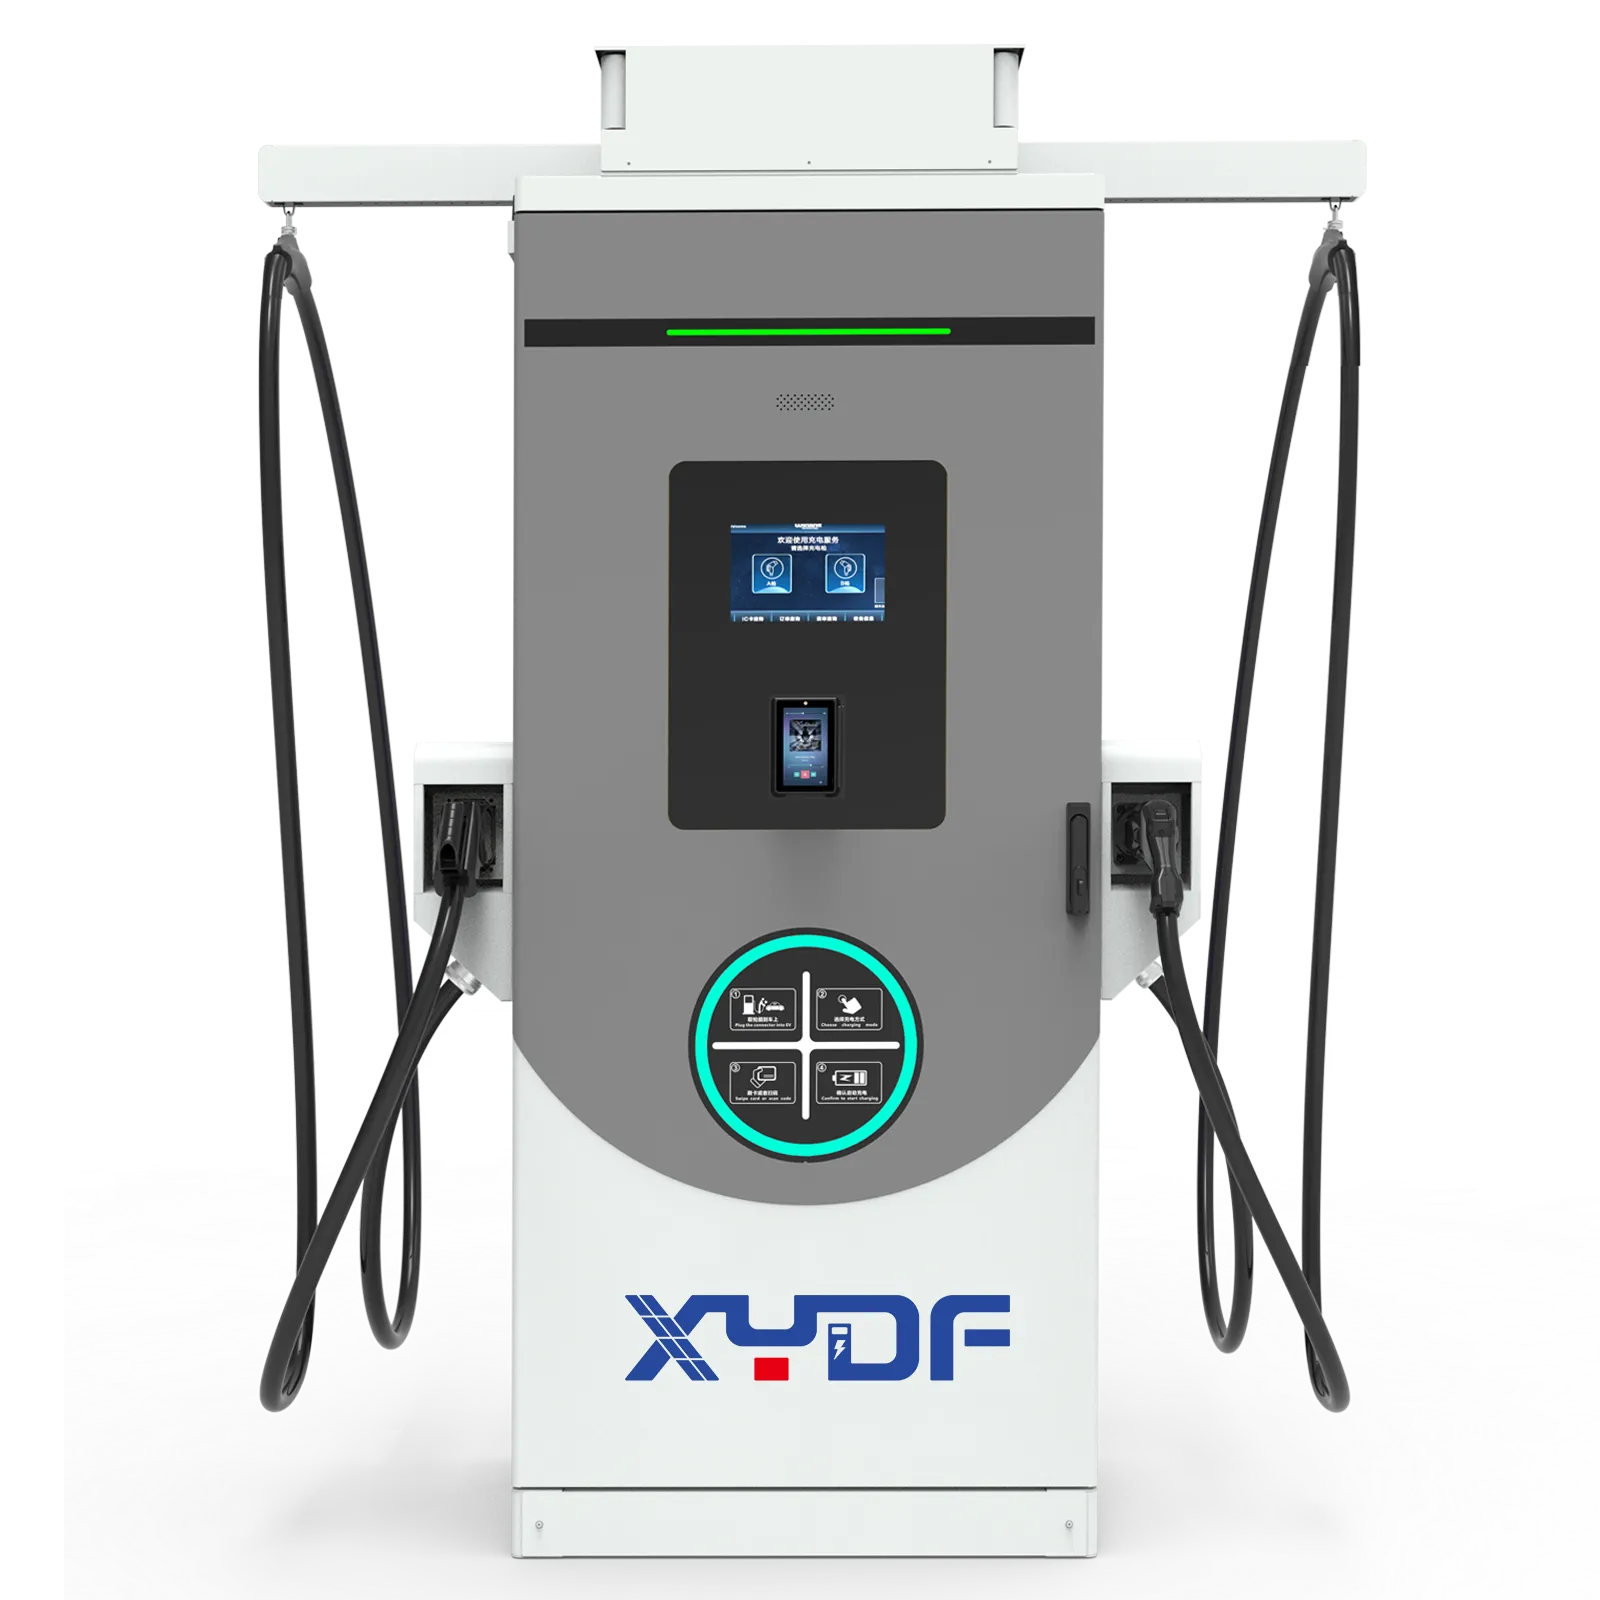
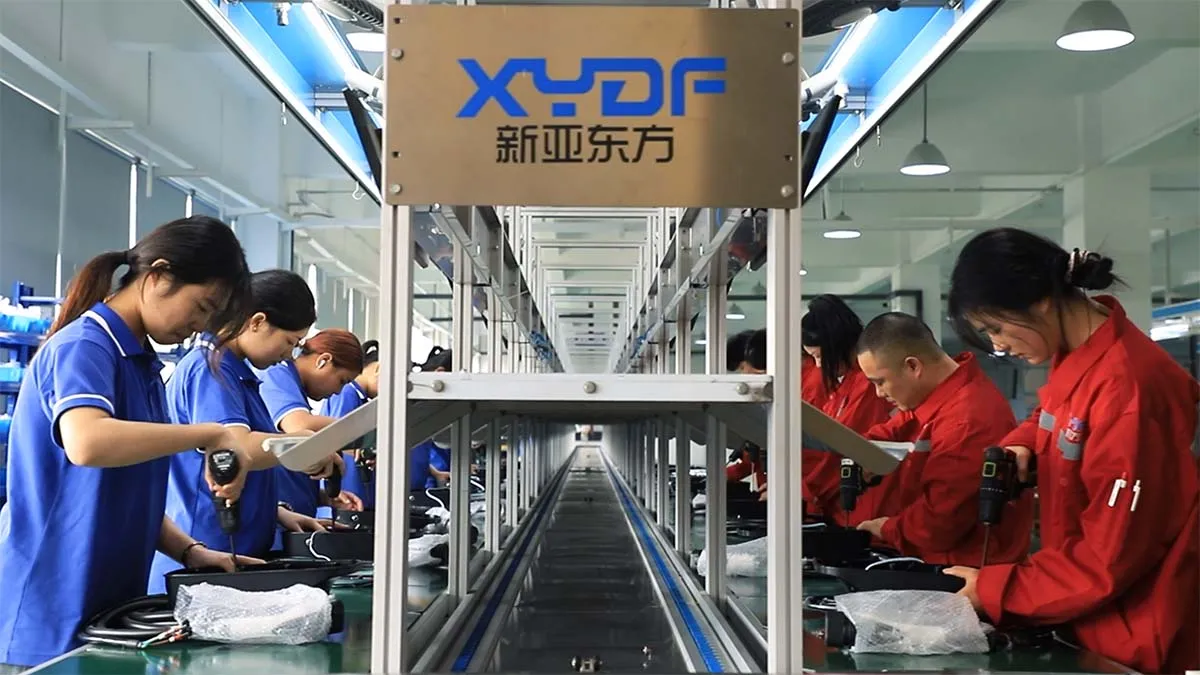
This factory walk-through helps buyers relate the audit checklist to real production areas and process flow.
Part 2. Which production areas should buyers inspect on site?
Commercial and fleet projects fail early when buyers discover too late that critical steps are outsourced. On-site review should map each manufacturing stage to a responsible team and record system.
Area
Pergunta de revisão
Porque é que isso importa
SMT / PCB production
Are control boards built and inspected under documented procedures?
Communication, safety, and billing logic depend on board quality
Power module integration
How are DC modules assembled, torqued, and inspected?
Power-path defects drive field failures
Cable and connector assembly
Are harnesses and gun assemblies tested for continuity and insulation?
Connector issues dominate warranty claims
Fuga de energia / envelhecimento
Is there a defined aging window and failure code log?
Screens infant mortality before shipment
Final inspection
Are safety, labeling, and accessory kits checked per traveler?
Prevents wrong market variant shipment
Packaging and logistics
Is impact protection and moisture control documented for export?
Reduces transport damage disputes
To determine whether a supplier manufactures or only assembles, procurement teams should walk each process area with traveler examples, not presentation slides.
How can buyers separate capacity claims from capacity evidence?
“Monthly capacity” can mean installed equipment, theoretical takt time, or finished units cleared for shipment. Ask for the definition, number of shifts, bottleneck operation, staffing assumptions, approved subcontractors, and a capacity plan for the planned ramp. This manufacturer capacity verification turns a sales claim into an auditable assumption.
Review recent travelers, then check whether test benches, burn-in space, and critical components can support the same volume. Do not convert a stated number into a guaranteed delivery promise without written allocation and recovery actions. Compare line records with the factory testing and incoming-inspection workflow to clarify what “100% tested” means.
Part 3. What quality records prove traceability and repeatability?
ISO 9001 or equivalent quality management is a starting point, but charger buyers need unit-level traceability from incoming components to final test results.
Record type
Minimum expectation
Review action
Incoming inspection
Component lots accepted/rejected with criteria
Sample 3 recent lots
Production traveler
Serial number linked to build steps
Trace one live serial end-to-end
Test log
Safety, communication, and functional results stored per unit
Match log to the sample serial
Corrective action
Defect categories, root cause, closure date
Check repeat defects over 90 days
Change control
Firmware/hardware revision approval flow
Confirm OTA and BOM revision governance
If a manufacturer cannot trace one finished charger back to PCB batch, module supplier, and test record, field failure analysis will be slow and warranty disputes will be harder to close.
What evidence should the audit team score?
Audit dimension
Strong evidence
Follow-up question
Incoming quality
Lot IDs, acceptance criteria, calibrated gauges, quarantine history
Can you trace this lot to finished units and returns?
Process repeatability
Controlled instructions, torque logs, change records
What changed after the last BOM or firmware revision?
Final testing
Per-serial safety, functional, communication, and thermal results
Which limits trigger rework, and who releases the unit?
Traceability
Serial linked to BOM, operator, station, test file, and shipment
Can you export the record without reconstruction?
Capacity
Defined units per shift, bottleneck plan, staffing, and allocation
What happens if demand doubles during ramp?
Service readiness
Spare-parts list, diagnostics, RMA, and corrective-action records
How are repeat failures escalated?
Part 4. Which functional tests should be demonstrated before shipment?
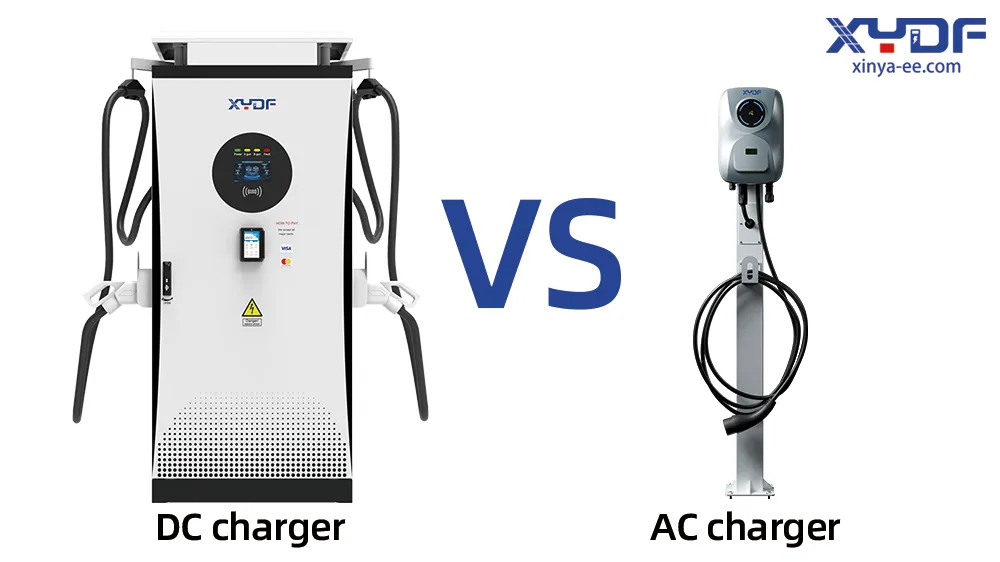
Test depth should match the product class. AC workplace chargers and high-power DC public chargers do not share identical test benches, but both need documented safety and communication validation.
Test category
AC commercial units
carregadores rápidos DC
Segurança elétrica
Insulation, leakage, ground continuity
Insulation withstand, HV interlock checks
Comunicação
OCPP session and fault reporting
OCPP, RFID/payment path, cooling telemetry
Thermal behavior
Heat-run under rated current
Module temperature and fan/pump response
Environmental
Ingress protection sample checks
Outdoor enclosure seal and corrosion controls
User interface
Language, payment, and access logic
Screen flow, connector lock, emergency stop
Request a demonstration on the exact firmware build and accessory configuration in your RFQ, not on a generic demo unit with different options. (OCPP EV charger guide)
Every charger should receive the defined safety and functional checks for its configuration; environmental qualification may be sample-based under an agreed plan. AC and DC products require different limits and fixtures, so “100% tested” is useful only when the supplier defines which tests run on every unit, which run by sample, and which acceptance limits trigger rework.
Part 5. How should buyers review certification and market compliance?
Certification evidence must match the destination market and the exact model family — not a sister product or outdated report.
Document
Verificação do comprador
Common gap
CE / CB / TÜV reports
Model name, power range, and standard edition
Certificate for different SKU
Label artwork
Voltage, current, and warning marks
Manual template reused across regions
EMC reports
Charger class and port configuration
Missing communication port configuration
Production consistency
Approved BOM tied to certificate sample
Silent component substitution
Why should buyers verify a standard’s scope instead of its logo?
ISO 9001 supports auditing documented processes, internal audits, corrective action, and continual improvement; it is not a product certification or uptime guarantee. IEC 61851-1 addresses conductive charging-system requirements and control functions, subject to edition and market rules. IEC 60529 defines IP-code test conditions; an IP claim does not cover corrosion, UV, impact, thermal cycling, or open-door operation.
Require the report scope, model, configuration, test setup, and laboratory details. That is the foundation of traceable EV charger production: the approved BOM, firmware, connectors, ports, labels, and power range must match the unit represented by the evidence. Unsupported or mismatched certification claims can delay market access, force retesting, or leave the buyer with a non-approved SKU.
XYDF publishes qualification evidence on the Qualificação page and manufacturing context on About XYDF. Compare those published routes with your RFQ target market before locking supplier approval.
OEM / ODM RFQ checklist
RFQ field
Why suppliers need it
Target models and power range
Maps platform and test scope
Connector standard and cable length
Affects certification and harness BOM
UI language and payment options
Drives firmware and labeling
OCPP version and backend target
Defines interoperability testing
Branding scope (OEM/ODM)
Determines tooling and packaging
Annual volume and lead-time window
Validates capacity allocation
Spare-parts and warranty terms
Sets service cost expectations
Part 6. Which XYDF platforms fit typical OEM and project routes?
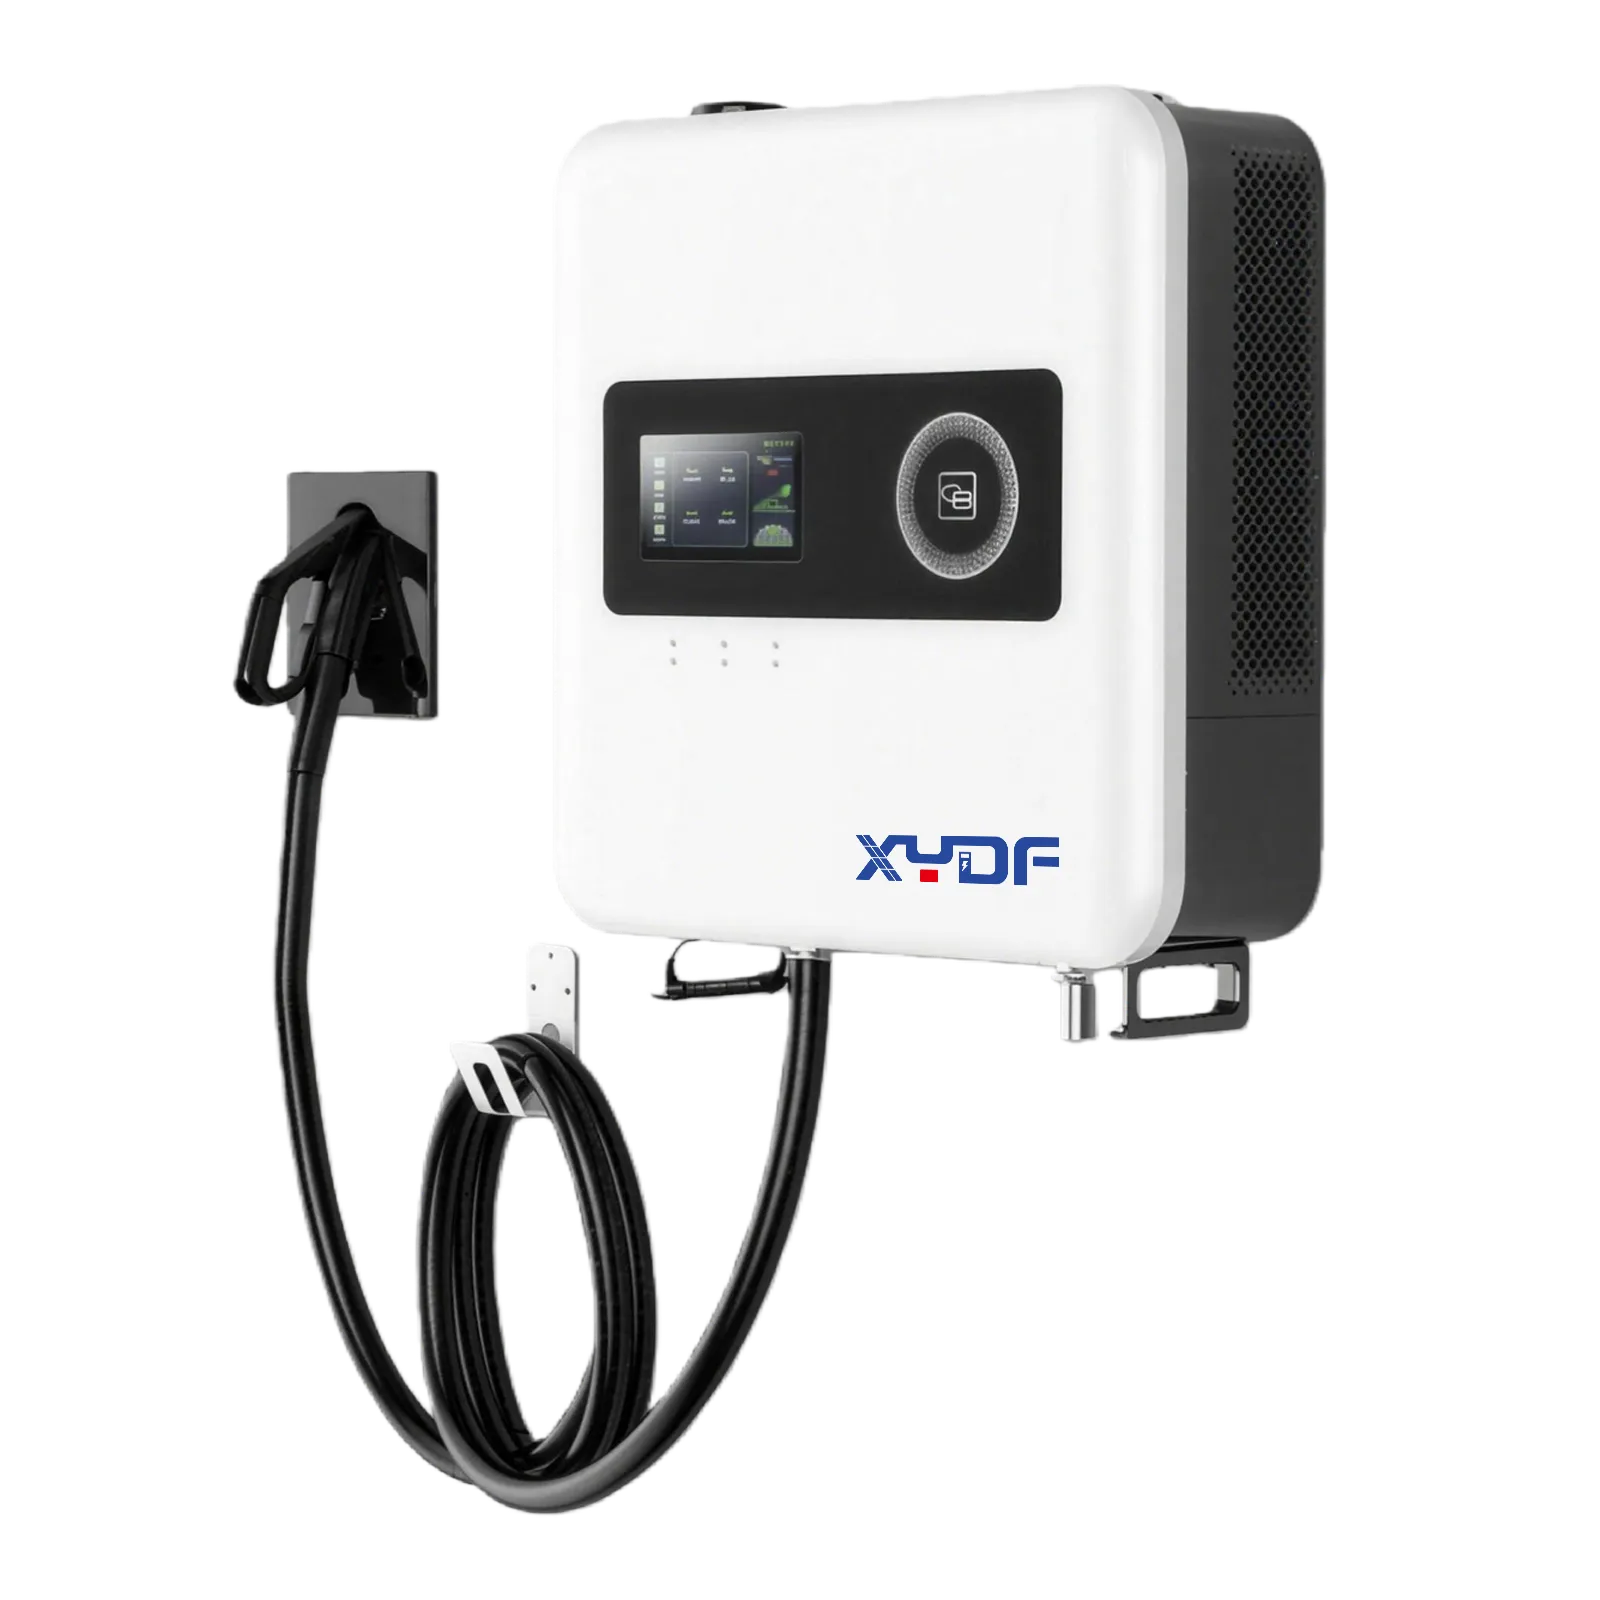
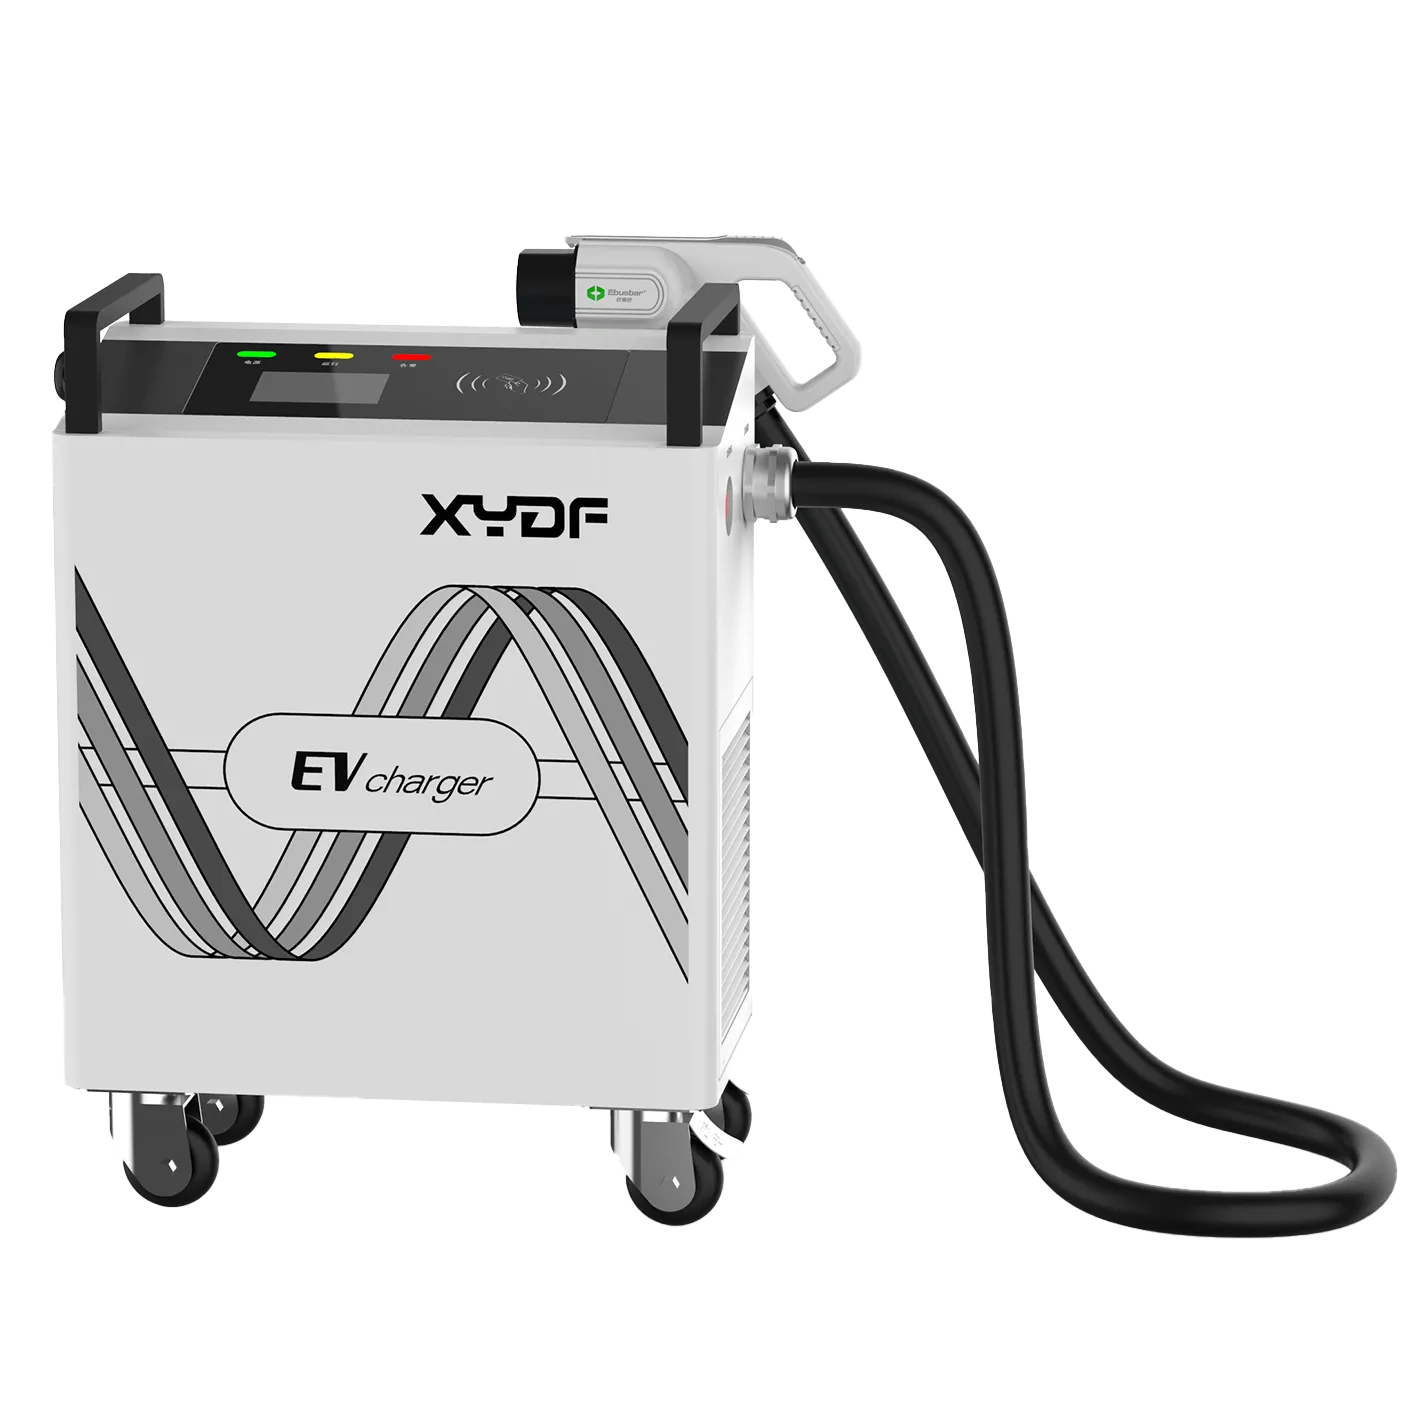
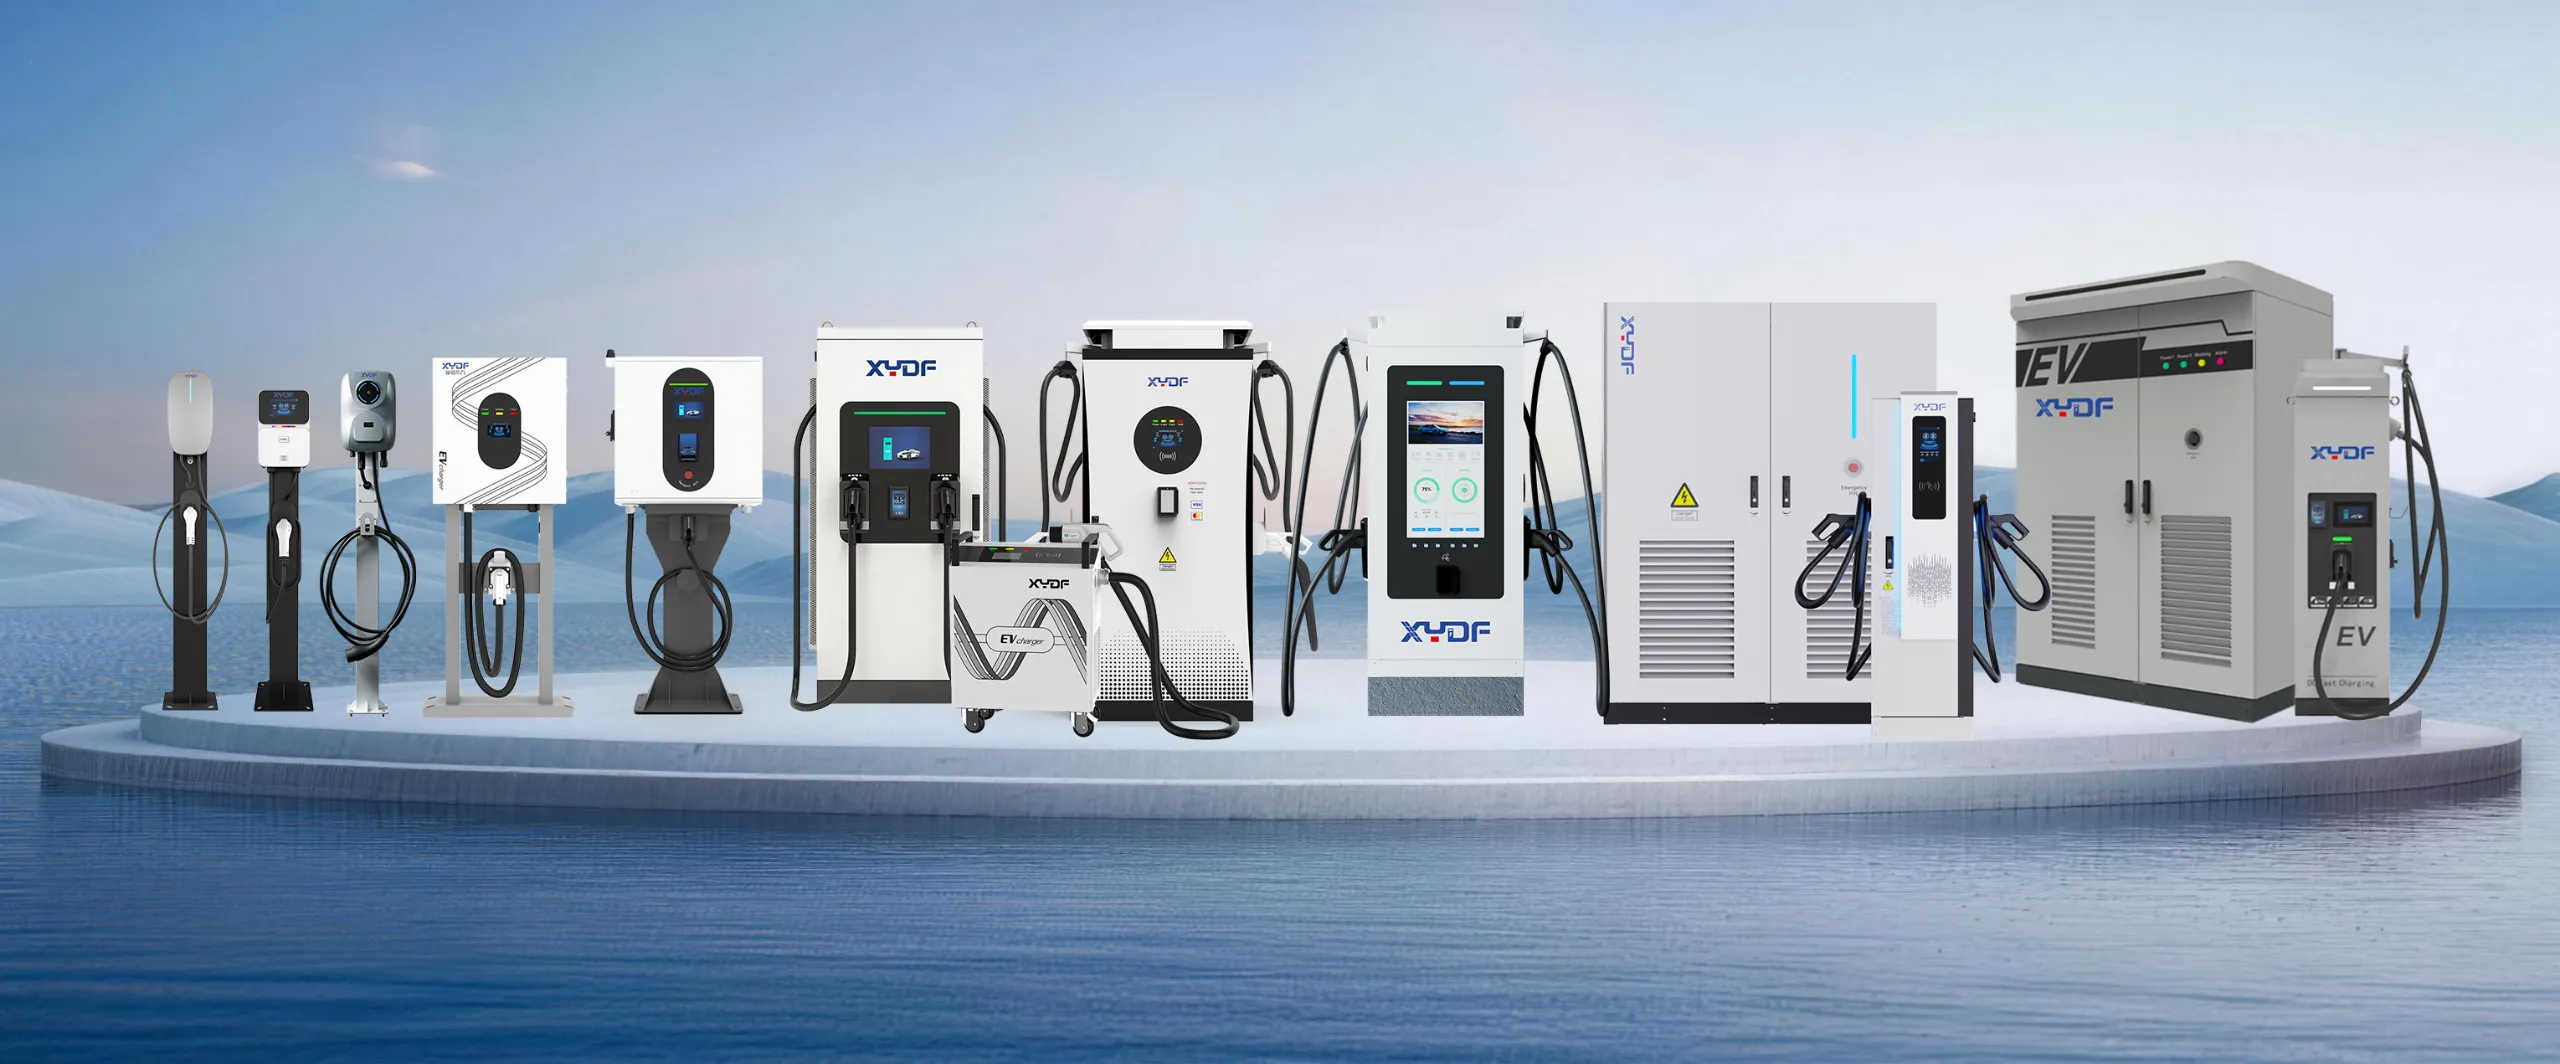
XYDF publishes commercial AC and DC platforms under Produtos with OEM/ODM support described on About XYDF. Use the audit checklist above before shortlisting any platform.
Buyer route
XYDF starting point
Audit emphasis
Workplace / destination AC
EC7 / EC22 / E22 series on /products/
Ingress rating, load management, OCPP
Compact commercial DC
EG / EYU / EEC1 series
Thermal design, module sourcing, screen options
High-throughput public DC
EC Series 80-240kW platform
Simultaneous power, service access, backend testing
Part 7. When is factory-audit approval incomplete?
This checklist supports supplier and platform selection for commercial and industrial EV charging programs. It does not replace:
On-site electrical design or grid capacity studies
Local wiring-rule compliance certification for every country
Payment network approvals or utility interconnection permits
Construction, civil works, or commissioning-only contracts
Price-only sourcing decisions without service scope
If a supplier refuses traceability records, will not demonstrate OCPP or safety tests on the RFQ configuration, or cannot align certification documents with the exact model ordered, treat approval as conditional—not complete.
What belongs in the procurement release checklist?
The approved model, power range, connector, and firmware revision match the RFQ and test records.
Incoming, in-process, final-test, rework, and change-control records are available for sampled serials.
Capacity is defined by shifts and bottlenecks, with component allocation and a ramp and recovery plan.
Applicable IEC 61851, IEC 60529, and destination-market requirements are mapped without unsupported certification claims.
Warranty, spares, diagnostics, response times, and data-access terms are signed; compare them with the B2B warranty-terms guide.
It is a structured review of production scope, quality systems, test capability, certification evidence, and service readiness before buyers place volume orders or launch OEM programs.
What production areas matter most during the visit?
SMT or control-board production, power module assembly, harness build, burn-in, final inspection, and export packaging — each should link to traveler and test records.
How can buyers verify an EV charger manufacturer’s capacity?
Ask how capacity is defined, then verify shifts, bottlenecks, staffing, test-bench throughput, component allocation, and recent travelers. A theoretical line rate is not a delivery commitment without written allocation and recovery actions.
Which documents should buyers request before approving a supplier?
Incoming inspection procedures, serial traceability examples, per-unit test logs, certification reports for the exact model, firmware revision records, and warranty/spare-parts terms.
What is the most important record in a factory audit?
Start with a complete serial trace linking incoming lots, build steps, firmware and BOM revision, test results, rework, and shipment. It shows whether the quality system works on real units rather than only in procedures.
Does ISO 9001 prove a factory makes reliable chargers?
No. ISO 9001 evaluates management-system and process controls. Product-specific tests, unit traceability, field feedback, and service commitments remain necessary.
How are OEM and ODM audits different?
OEM programs stress branding, packaging, manual language, and revision control. ODM programs add design ownership questions around enclosure, firmware, and certification responsibility.
What tests should be demonstrated for DC fast chargers?
Insulation withstand, communication sessions, thermal behavior, connector lock logic, emergency stop response, and cooling telemetry should be shown on the RFQ configuration.
Should every charger receive the same tests?
Every unit should receive the safety and functional checks defined for its configuration; environmental qualification may be sample-based under an agreed plan. AC and DC products need different limits and fixtures, so buyers should confirm the per-unit and sample-based test matrix.
When should a buyer reject an EV charger manufacturer?
Reject or pause approval when certification scope does not match the ordered SKU, traceability is missing, critical production is undisclosed outsourcing, capacity definitions shift, test scope is unclear, or service and spare-parts commitments are undefined. Agree corrective actions, owners, and verification dates before volume release.
Can this checklist replace a third-party factory inspection?
No. It defines technical and quality evidence buyers should demand. Third-party inspections still help when project value, new supplier relationships, or compliance risk warrant independent verification.
A factory audit turns confidence into checkable evidence: one unit, one record, one accountable owner. If your RFQ needs a documented review of process, capacity, and service risk, Entre em contato com XYDF with the target market and production volume.
Como um comprador pode conectar a evidência da fábrica à aceitação no terreno?
Relacione cada controle de fábrica a um requisito de campo: identifique o modelo e a versão testados, defina o método de teste e os critérios de aprovação, mantenha registros de calibração e defeitos e repita os verificamentos críticos durante a aceitação do local com a configuração entregue. Uma visita guiada ou um certificado são contextos úteis, mas a cadeia verificável é a configuração, a evidência e o resultado testemunhado.
Fábrica da Sede em Zhejiang:
N.º 2, Estrada Changjiang, Parque Industrial da Ponte de Wenzhou, Vila de Beibaixiang, Cidade de Yueqing, Cidade de Wenzhou, Província de Zhejiang
Escritório de Shenzhen:
1.º Andar, Edifício A, Parque Industrial de Shenkai, Comunidade de Tangtou, Subdistrito de Shiyan, Distrito de Bao'an, Shenzhen
Utilizamos cookies para manter este site a funcionar e, com a sua permissão, para medir a forma como os visitantes utilizam o nosso site de carregamento de VE. Consulte os nossos Política de Privacidade para mais detalhes.
 Xinya Dongfang Electricity Technology Co., Ltd.