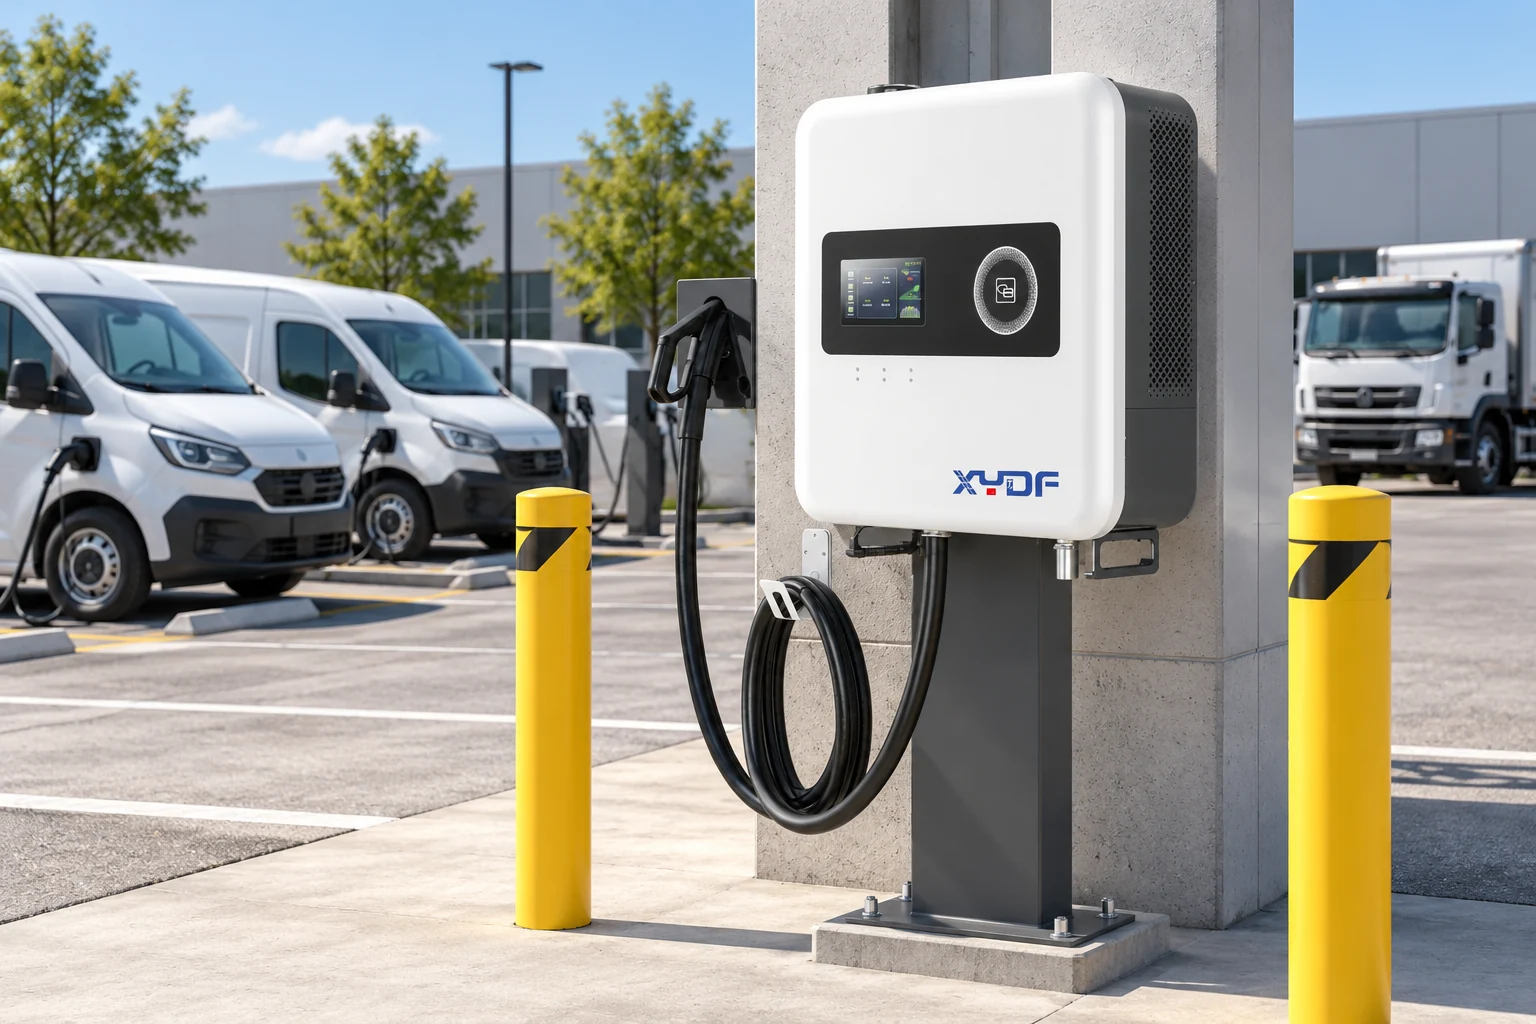
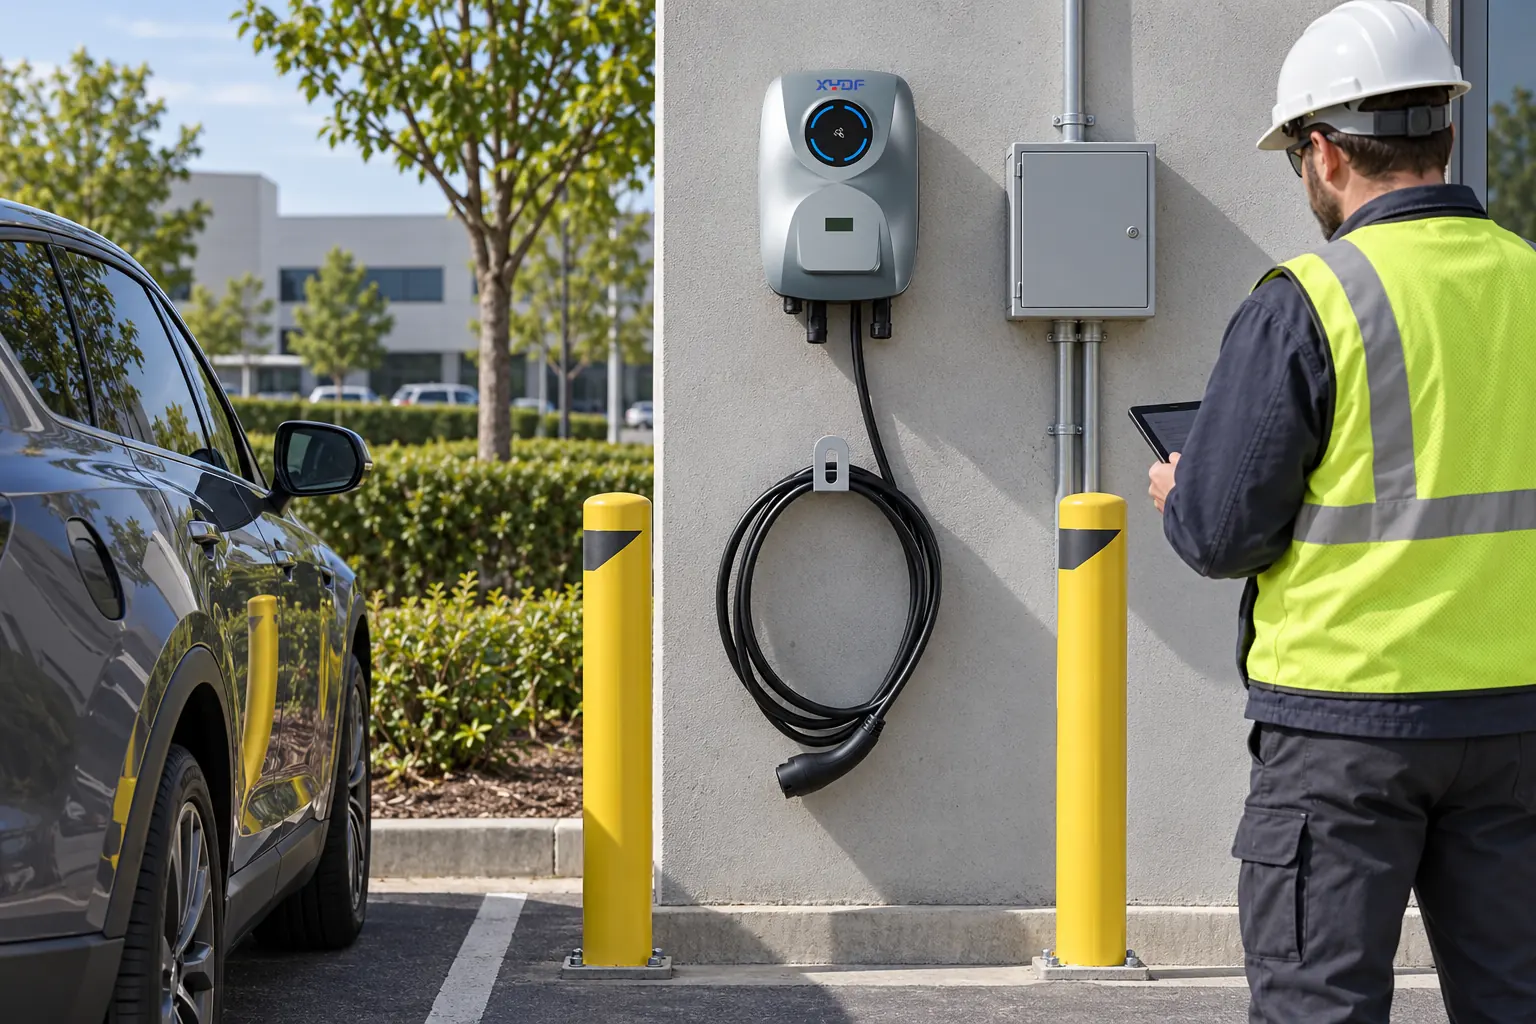
From Sample to Mass Production: The DFM Process for Custom EV Chargers
Juil 26,2026
Blog
A charger sample can pass functional checks and still expose production problems during the first pilot, including pinched harnesses, inaccessible service screws, and fixtures that do not support repeatable assembly. A staged DFM review turns those findings into drawing changes, accessible test points, and a controlled release.
custom EV charger DFM process—treat design for assembly, tolerances, thermal behavior, EMC, connectors, and serviceability as gated work before tooling and volume release. EVT asks whether the concept works, DVT whether production-representative units meet requirements, and PVT whether the line can repeat the build. IEC 61851, IEC 62196, and relevant IEC 61000 parts may define charging-system, connector, and EMC requirements; confirm the applicable editions and market deviations in the contract.
Between an approved sample and mass production sit three validation gates—EVT, DVT, and PVT. Projects that skip or compress them tend to pay later through tooling rework, certification surprises, unstable yield, or field failures. The aim is not merely to build one working unit, but to make a factory capable of building thousands of consistent units under controlled documentation.
What Does DFM Change Between a Charger Sample and a Production Unit?
Un audit fournisseur est plus utile lorsque chaque déclaration de l’usine est liée à un document ou à un contrôle témoin. Traquez la configuration du produit depuis l’inspection initiale jusqu’à la mise à jour du firmware ou de l’équipement, en passant par les contrôles de processus, les tests finals, le traitement des non-conformités, la calibration, le contrôle des changements et la libération des envois. Cela crée un parcours d’approvisionnement prêt à être cité sans supposer que la seule visite dans l’usine prouve les performances sur le terrain. Pour le contexte de planification publique, voir Exigences du système de charge conductif IEC 61851-1; Le dossier d’acceptation site-spécifique reste le facteur déterminant de la décision finale.
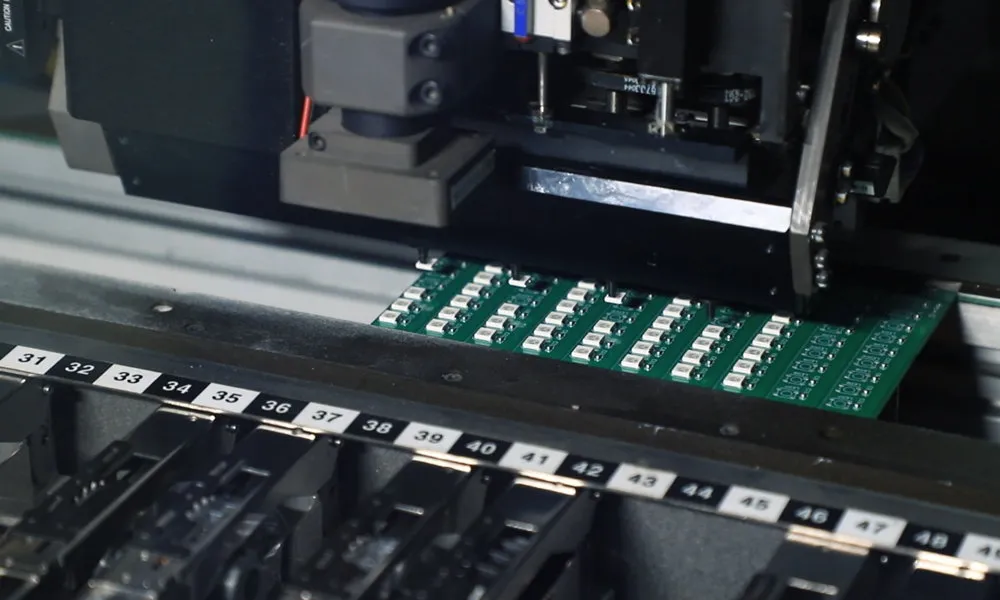
Design for manufacturing adapts a working design so it can be produced repeatably and economically. Part counts may fall, tolerances must match real process capability, assemblies need to follow the order in which a line can build them, and test points have to sit where fixtures can reach them. A hand-built sample proves the concept; DFM proves the concept survives other people building it.
This is also design for assembly and service. The work covers assembly sequence, fastening, materials, test access, serviceability, and controlled changes—not just the enclosure or printed circuit board. A design that can be assembled only by the engineer who developed it is not ready for production.
The economics move in one direction. Findings are comparatively easier to address while the design is still flexible and become expensive after hard tooling, certification work, and production documentation are locked. That is why industrialization guides place manufacturability review before design freeze. Whether the program uses an OEM or ODM structure also determines who owns drawings, firmware, validation work, and later changes; the OEM-versus-ODM buyer guide maps that choice.
Cofactr’s analysis of the prototype trap gives this example: “A connector that needs a wiggle at low volume can become a 4% failure rate, and a 30-second expert assembly step can become a three-minute production bottleneck.” It explains why pilot builds must operate as production rehearsals.
How Do EVT, DVT, and PVT Structure a Custom Charger Program?
A structured program replaces one vague “sample approval” with EVT-DVT-PVT validation gates, each answering a different buyer question. The EMS handbook’s NPI stage-gate model treats the gates as pass/fail decisions supported by defined evidence.
Porte
Question de l'acheteur
Typical build
Required evidence
EVT—engineering validation
Does the architecture, design, and safety concept work?
Small hand-assembled or soft-tooled batch
Risk register, early schematics, and representative charging and protection tests
DVT—design validation
Is the frozen design reliable, compliant, buildable, and suitable for its market?
Production-grade materials and near-final tooling
Production-intent materials, tolerance stack, environmental and EMC plans, and updated drawings
PVT—production validation
Can the line build the approved design consistently and at the agreed yield?
Pilot run on mass-production tooling and fixtures
Tooling and fixtures, work instructions, pilot yield and cycle-time records, and final-test logs
Mass production / MP release
Can the full line repeat at volume while changes and suppliers remain controlled?
Full line under controlled documentation
Approved BOM, revision sign-off, control plan, and nonconformance and change workflows
Every gate needs written exit criteria and a named approver. As one NPI process guide puts it, “‘Looks good’ is not” a gate. Large bill-of-materials changes late in DVT require another DVT pass before PVT begins, because operators, fixtures, and test equipment must be shown to repeat the revised result.
What Must DVT Prove Before Tooling and Certification Spend?
DVT is where the design meets reality on production-representative units. It covers environmental and reliability stress, mechanical fit, safety margins, thermal behavior, electromagnetic compatibility (EMC), connector performance, service access, and the compliance evidence required for the destination market.
For an EV charger, the base conductive-charging requirements sit in IEC 61851-1, while IEC 62196 may apply to plugs, socket-outlets, vehicle connectors, and vehicle inlets. IEC 61000 is a family of EMC emission, immunity, and test-method standards, not one blanket product certification. The contract therefore needs to identify the relevant parts, editions, national deviations, product configuration, intended use, and market rather than say only “complies with IEC.”
Which hidden failure modes deserve a DFM review?
Tolerance stack: calculate worst-case or statistical stack-ups for doors, gaskets, busbars, connector alignment, and mounting holes. Mark critical dimensions and inspect them with calibrated tools.
Thermal path: check contact pressure, interface materials, airflow, fan or pump access, derating logic, and hot-spot measurements at rated load. Test the enclosure and harness as assembled, not as isolated parts.
EMC: map cable routing, shields, bonding, filter access, and grounding so the production build matches the configuration evaluated for EMC. Select the applicable IEC 61000 parts for the charger and market.
Connector and cable: verify keying, insertion force, locking, strain relief, bend radius, pin mapping, sealing, and replacement access. Confirm the exact IEC 62196 interface and edition where that series applies.
Serviceability: time the safe replacement of fans, contactors, power modules, cables, and control boards; provide diagnostic points, torque values, and firmware recovery steps. A part that cannot be reached without disturbing sealed safety barriers creates lifecycle risk.
Qu'est-ce que chaque type d'évidences de la TVP apporte réellement en réalité ?
Evidences
What it proves
What it does not prove
3D model and tolerance stack
Parts can fit within stated variation
Operators can assemble them at rate
Thermal run on a production-intent unit
Heat-path and derating assumptions under the defined load
Long-term reliability in every climate
EMC test plan and results
Applicable IEC 61000 tests were scoped and performed
Compliance of an altered harness or firmware revision
Connector validation
Interface, sealing, locking, and service actions work together
Vehicle interoperability outside the tested matrix
PVT records
The line, fixtures, and instructions can repeat the approved build
Future revisions remain equivalent without change control
Certification timing is a planning decision. Testing an EVT-grade prototype can waste laboratory budget if the design then changes; waiting until tooling is locked can make a failure expensive to correct. Begin risk reviews in EVT, then perform production-intent thermal and EMC validation during DVT before certification or hard tooling is fixed. Re-run the impact analysis when the enclosure, harness, power module, connector, or firmware changes.
Programs that pass DVT cleanly are more likely to become reliable fleets. The connection between validation records and field performance is covered in the guide to evaluating EV charging equipment reliability.
What Does PVT Prove, and What Resets Validation?
PVT validates the factory process for the approved design. Run the pilot with production-intent tooling, operators, fixtures, software, packaging, and inspection plans. Measure first-pass yield, rework categories, cycle time, work-instruction clarity, fixture behavior, test escapes, torque or leak failures, traceability, packaging, and field-simulation results. Report counts and definitions against the approved control plan instead of inventing a universal target percentage, and record who accepted every deviation.
First-pass yield matters because low yield can hide rework behind units that eventually pass. That points to process instability, variable quality, and schedule risk that may later reach the field. Stage-gate references therefore use explicit PVT targets, including first-pass-yield thresholds and statistical control of critical dimensions, but the actual acceptance values belong in the specific program agreement.
Hubble Network’s pre-production testing guidance states: “Any design change during PVT resets you to DVT. Full stop.” At minimum, any change affecting safety, compliance, form-fit-function, thermal behavior, EMC, the connector interface, firmware, tooling, or a service procedure needs documented impact analysis and may require DVT or PVT to be repeated. A supplier that quietly edits the design during the pilot creates a schedule and quality risk.
After DVT freeze, classify every proposed change by safety, compliance, form-fit-function, firmware, tooling, and supply risk. Require updated drawings and BOM records, regression tests, approval, and revision traceability before the change reaches PVT or mass production. A component substitution without EMC, thermal, connector, and certification review can invalidate earlier evidence.
The pilot also stress-tests the production quality-control system: incoming inspection, in-process checks, burn-in, and end-of-line testing. Use the incoming and factory testing workflow to assess those controls.
Which DFM Checkpoints Belong in the Contract?
A custom program can drift quietly, so buyers should place the gate logic, evidence, ownership, and change rules in the purchase agreement. The following EV charger supplier DFM checklist turns “sample approved” into auditable decisions.
Buyer should specify
Required detail or evidence
Pourquoi c'est important
Base platform versus clean-sheet design
Custom delta list, target markets, connector standard, power range, software/backend, and ownership of drawings and firmware
Sets which validation history can be inherited and which work must run fresh
Applicable standards and certification plan
Map IEC 61851 requirements, IEC 62196 interfaces, relevant IEC 61000 parts, editions, national rules, model, and destination market
Places the correct compliance work inside DVT without implying an unsupported certification
Written exit criteria for every gate
Named approver; tests, yield, and documents; risk register, tolerance analysis, thermal and EMC plans, connector drawings, and service procedure
Converts “looks good” into evidence
Pilot-run scope and acceptance
Pilot size and configuration, measurement methods, yield and rework definitions, serial traceability, deviation approval, cycle time, and final-test records
Defines what PVT must prove before volume units ship
Change control after DVT freeze
Lock the approved BOM, test limits, tooling, packaging, and firmware revision; require impact review and approval for substitutions
Stops late churn from resetting the schedule invisibly or carrying old approvals forward
Capability verification belongs beside the documents. Real NPI discipline is visible on the factory floor, in change records, and in retained samples. The EV charger factory audit checklist is designed to test that evidence. Buyers can also use the Guide d’achat de chargeurs pour véhicules électriques to align the DFM matrix with commercial terms.
How Should Buyers Scope a Custom Program With XYDF?
Many “custom” charger programs do not need clean-sheet hardware. Starting from a validated platform and defining only the necessary changes—such as enclosure branding, interface languages, connector and power configuration, and market-specific options—can preserve relevant validation history while still producing a differentiated product. It is generally the faster, lower-risk starting point, provided the supplier documents which evidence remains applicable.
XYDF states on its official site that it has a 20+ engineer R&D team and four product generations, and its catalog covers AC and DC platforms. Buyers can review the XYDF EV charger product range et le EG Series 40kW DC fast charger as one compact-platform example.
Send the custom delta list, target market, connector and power requirements, and proposed gate criteria through the XYDF contact page. The discussion should identify which stages and records the program can inherit and which tests must be run again. This guide is for buyers commissioning customized chargers and auditing supplier NPI discipline; it does not state XYDF program timelines, yields, or costs, and it does not replace target-market certification testing.
Custom EV Charger DFM FAQ
Qu’est-ce que DFM pour un chargeur EV personnalisé ?
Le design pour la fabrication adapte un design approuvé afin que les personnes, les outils, les dispositifs et les essais puissent le construire à plusieurs reprises. Il modifie les quantités de pièces selon les besoins, les tolérances, les matériaux, la séquence d’assemblage, les fixations, l’accès aux essais, la réparabilité et la manière de contrôler les modifications.
Qu'impliquent EVT, DVT et PVT pour une commande de chargeur personnalisé ?
EVT prouve que le concept de conception et de sécurité fonctionne ; DVT vérifie la fiabilité, la conformité et la manufacturabilité des unités de production ; PVT démontre que la ligne de production peut réaliser la configuration approuvée avec le rendement et le cycle de production convenus. Les trois volets permettent de séparer les risques liés au concept, au design et au processus.
Quand doivent-elles se dérouler les vérifications thermiques, EMC et de certification ?
Commencez les évaluations des risques thermiques et électromagnétiques dans le cadre de l’EVT, puis vérifiez-les sur des unités destinées à la production lors du DVT. Les essais de certification doivent être suffisamment avancés pour que le design soit stable, mais suffisamment prématurés pour que l’incident ne contraigne pas à une réusinage inévitable ; réévaluez les preuves lorsque les modifications concernent l’enceinte, le harnais, le module d’alimentation, le connecteur ou le firmware.
Qu’est-ce qu’une production pilote de PVT devrait mesurer ?
Il devrait mesurer le taux de recyclage des pièces, les catégories de retouches, le temps de cycle, le comportement des accessoires, les fuites lors des essais, la traçabilité, le rendement des instructions de travail et l’emballage avec des définitions convenues. Les opérateurs, les outils, les accessoires, le logiciel, le plan d’inspection et la configuration de la ligne destinés à la production en série doivent être représentés.
Pourquoi le taux de première passation importe-t-il aux acheteurs ?
Un faible taux de recyclage signifie que les modifications peuvent être cachées derrière des unités qui finissent par passer. Cela indique un processus instable, une qualité variable et un risque de dépassement du calendrier qui peuvent se manifester sur le terrain ; il est donc nécessaire que le contrat définisse à la fois l’objectif et la manière dont les modifications sont comptabilisées.
Comment les normes IEC 61851 et IEC 62196 diffèrent-elles ?
La norme IEC 61851 traite des exigences relatives aux systèmes de charge conducteurs ainsi que des fonctions de contrôle. La norme IEC 62196 traite des prises, des bornes de connexion, des connecteurs de véhicule et des entrées de véhicule ; applique les éditions correspondantes et les règles nationales aux interfaces et aux marchés de destination respectifs.
Qu’est-ce que l’IEC 61000 signifie pour un projet de chargeur pour véhicules électriques ?
Le IEC 61000 est une famille de normes EMC couvrant les émissions, l’immunités et les méthodes d’essai. Une demande de propositions devrait indiquer les éléments applicables et la configuration d’essai plutôt que de considérer “ IEC 61000 ” comme une certification unique.
What happens if the design changes during PVT?
The strict approach is to return to DVT because the pilot no longer represents the design being sold. In all cases, a change affecting safety, compliance, form-fit-function, thermal behavior, EMC, connector interface, service procedure, firmware, or tooling should trigger documented impact analysis and may require DVT or PVT to be repeated; the contract should make this rule explicit.
Comment un acheteur peut-il associer les preuves de l’usine à l’acceptation sur le terrain ?
Lier chaque contrôle de la chaîne d’approvisionnement à une exigence de terrain : identifier le modèle et la version testés, définir la méthode d’essai et les critères de réussite, conserver les données d’étalonnage et les registres de défaillance, et répéter les contrôles critiques lors de l’acceptation du site avec la configuration livrée. Une visite guidée ou un certificat sont des éléments utiles, mais la chaîne vérifiable est constituée par la configuration, les preuves et les résultats constatés.
A sample proves intent; disciplined DFM proves repeatability. For a gate plan covering a custom AC or DC charger, Contacter XYDF with the delta list, target market, and pilot criteria.
Usine du siège social du Zhejiang :
N° 2, route de Changjiang, parc industriel du pont de Wenzhou, ville de beibaixiang, ville de Yueqing, ville de Wenzhou, province du Zhejiang
Bureau de Shenzhen :
1er étage, Bâtiment A, Parc Industriel Shenkai, Communauté Tangtou, Sous-district de Shiyan, District de Bao'an, Shenzhen
Nous utilisons des cookies pour assurer le bon fonctionnement de ce site Web et, avec votre autorisation, pour mesurer la manière dont les visiteurs utilisent notre site de recharge pour VE. Voir notre Politique de confidentialité pour plus de détails.
 Xinya Dongfang Electricity Technology Co., Ltd.